Specifying custom walk-in closet organizer system suppliers for Wholesale and OEM Orders
The limiting factor is rarely the headline specification; it is whether a second supplier can reproduce the same panel dimensions, hole positions, edge finish and hardware fit across repeat orders. A small mismatch can turn a modular closet into a site adjustment, with installers trimming panels or shifting rails to recover alignment.
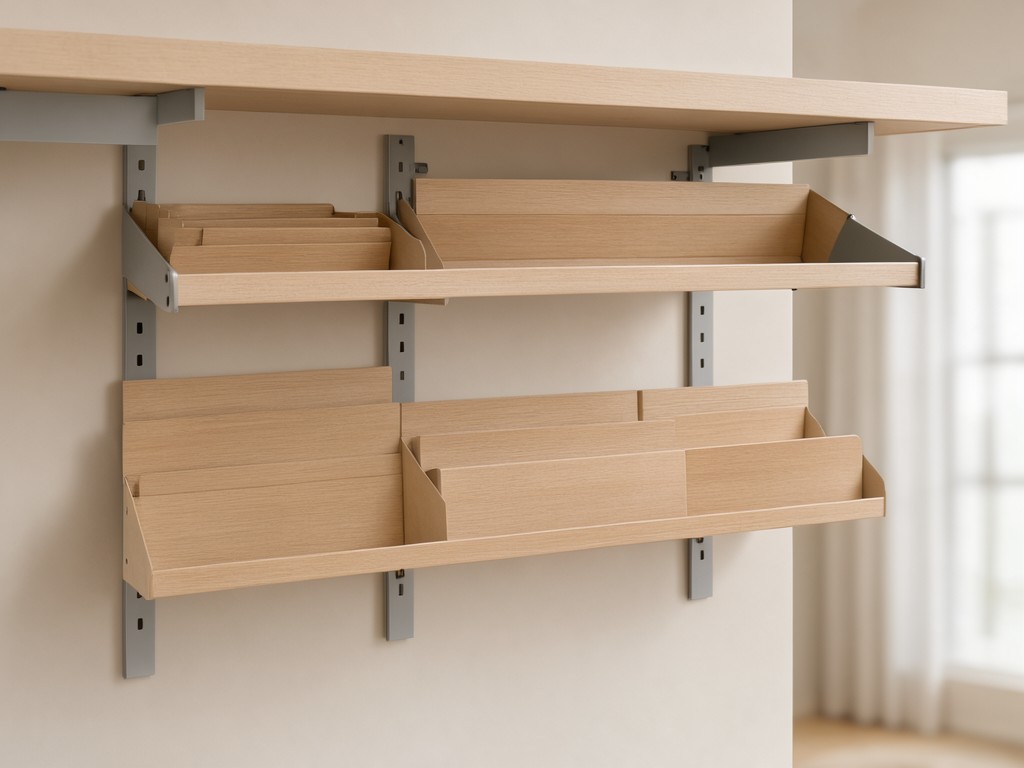
Fatigue appears at the stress concentration: around shelf supports, drawer runners, rail brackets and fastener points. Material thickness alone does not resolve it. Buyers qualifying custom walk-in closet organizer system suppliers should compare substrate, edge protection, support spacing and hardware interfaces against the intended load and cleaning routine, then approve a sample built to the same specification as production.
What the Design Has to Balance
Weight and stiffness trade off against each other. Thicker panels and closer supports reduce shelf deflection, but add material cost, carton weight and handling effort. The right choice follows the shelf span, stored load and installation method rather than a single panel-thickness target.
For a cleanable interior, sealed edges and a wipeable face matter more than a claim of general weather resistance. UV exposure near a window can fade some decorative finishes; damp clothes, perspiration residue and occasional swimwear can leave moisture or salts at seams. Specify a finish and edge treatment for those conditions, and keep standing water or unapproved chlorine cleaners out of the care instructions.
Comfort is also physical: rounded exposed edges, smooth drawer travel and secure rail connections reduce snagging and rattling during daily use. A more substantial hardware set may raise unit cost, but can make sense for high-turnover closets where doors and drawers see frequent cycles.
How It Performs in Use
Usage level changes the load pattern and cleaning burden. Use the comparison to align construction with the customer’s actual closet routine; final shelf spans, support locations and hardware should be confirmed in the approved layout.
| Usage level | Typical stress and care | Specification direction |
|---|---|---|
| Private household, daily access | Regular hanger contact, drawer use and dry-cloth or damp-cloth cleaning. | Prioritize smooth edges, consistent drawer clearances and a face finish suited to routine wipe-downs. |
| Shared household or high-turnover rental | More frequent opening, heavier mixed storage and less controlled cleaning habits. | Review support spacing, runner selection, edge sealing and replacement-part availability. |
| Closet storing sportswear or swimwear | Perspiration residue, damp garments or trace chlorine on stored items can reach shelves and drawer interiors. | Specify sealed panel edges and clear care guidance; dry wet items before storage and avoid harsh cleaners unless finish compatibility is confirmed. |
A closet organizer is an indoor system, not an exterior cabinet. For installations exposed to direct sun, repeated damp storage or aggressive cleaning, confirm the face material, edge treatment and care limits before locking the finish for bulk production.
How It Is Built and What That Changes
A common construction route combines cut-to-size melamine-faced particleboard or MDF panels with edge banding, pre-drilled connector patterns, metal hanging rails and purchased drawer or wardrobe hardware. A supplier may also offer plywood panels or aluminum and steel frame elements; those choices change weight, cost, visual feel and how the system is fixed to the room.
Panel processing typically runs through cutting, edge application, drilling and hardware preparation before the parts are checked against the assembly drawing and packed by module. Powder-coated metal components require their own finish and fit control. For a second-source qualification, compare the actual drilling map, edge profile, connector set and rail interface—not only the material description on the quotation.
Tighter edge and drilling control costs more than a basic cut-and-pack build, but lowers the risk of visible substrate at exposed edges and assembly problems at installation. Confirm which dimensions are fixed by the supplier’s tooling and which can be adjusted to your room plan before approving the first sample.
What Can Be Customised and What Cannot
Layout, finish and packaging are usually the main private-label decisions. The supplier still needs a defined system envelope: panel thickness, connector geometry, rail interface and hardware clearances must remain compatible within each approved configuration.
Flexible by Project
Module widths, shelf and drawer arrangement, rod placement, decorative finish, edge colour, handle choice, labels and carton artwork can often be set to the buyer’s range. Custom surface colours or printed packaging may carry material minimums or longer purchasing windows.
Fixed by Compatibility
Connector positions, runner clearances, rail dimensions and panel thickness cannot be changed in isolation without revising mating parts or the assembly drawing. Treat these as controlled system dimensions, not cosmetic options.
| Customisation area | Buyer can specify | Constraint to confirm |
|---|---|---|
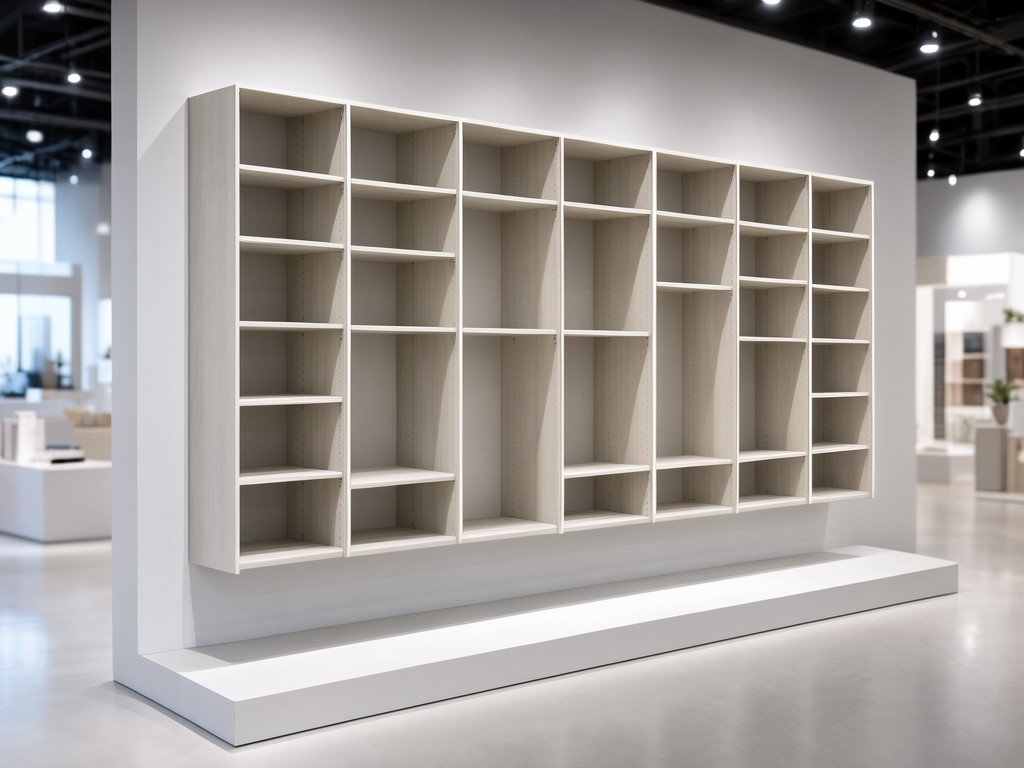
| Layout and module sizing | Shelf, hanging, drawer and corner-unit combination; target installation dimensions. | Room measurements, wall fixing method, span support and the supplier’s cutting limits. |
| Panel and metal finish | Available panel substrate, face pattern, edge band, rail material and coating colour. | Finish availability, colour matching, surface-care limits and any supplier minimums. |
| Hardware and branding | Drawer hardware, pulls, product labels, instructions and carton graphics. | Hardware fit within the approved layout; artwork files, language versions and packaging quantities. |
Quality Control and Batch Consistency
For a second source, control the details that determine interchangeability: finished panel dimensions, hole locations, edge-band coverage, rail length, hardware identity and colour reference. Keep the approved drawing, bill of materials, finish sample and carton specification tied to the same revision so a reordered module does not drift from the launch batch.
Agree how the supplier records lot-level material and hardware changes, and require written approval before substitutions. A lower-cost panel or alternate runner may look similar in a sample but change the assembled feel, edge appearance or fit. Clear acceptance criteria help procurement compare quotes without leaving production teams to interpret finish or fit by eye.
Packaging is part of batch consistency too. Specify protection for exposed corners and finished faces, identify each carton by module, and match labels to the installation sequence. That reduces mix-ups during distribution and limits abrasion damage in storage and transit.
Volume Planning and Lead Time
Lead time depends on panel and hardware availability, finish selection, sample approval, drawing changes and the pack configuration. Standard finishes and existing hardware generally simplify replenishment; custom colours, new components or revised drilling patterns add approval and purchasing steps.
For a second-source launch, separate sample quantities from the first production order and confirm the minimums for each custom item, not only the assembled system. Forecast by repeatable module and finish combination so the supplier can plan materials without forcing excess stock in slow-moving options.
Request a Production-Representative Sample
Send the target layout, finish reference, hardware requirements, carton plan and expected order mix with the sample request. Ask the supplier to build from the proposed production materials and drilling configuration, then use the approved sample as the reference for repeat orders.